Steel Casting Vendor: What to Look for Before You Commit
2026-10-29
Every steel casting buyer has a horror story: a vendor who promised tight tolerances, then delivered porosity-riddled parts. The difference between a smooth production run and a stalled line often comes down to what you verify before signing. At Supreme Machinery, we believe the foundation of a reliable partnership is knowing exactly what to look for—from metallurgical testing to lead-time honesty. This guide walks you through the non-negotiables before you commit.
Dig Into Their Melt Chemistry, Not Just the Quote
Any vendor can hand you a spec sheet and a per-part price. But the real story lives in how the polymer flows when things get hot and fast. Ask to see actual melt flow data from their production runs, not just a lab sample. A molder who tracks viscosity shifts across multiple lots—and adjusts barrel temps or screw speed accordingly—will save you from brittle parts and surprise tool wear down the line.
Look for signs they treat melt chemistry as a living variable, not a set-and-forget parameter. Do they run purge protocols between material changes? Can they explain how moisture levels, regrind ratios, or colorant loads affect your specific resin's flow front? If the conversation never moves past “it meets the datasheet,” you're probably talking to someone who buys pellets, not someone who understands them.
Finally, ask for a real-time example: a project where they caught a melt flow deviation mid-production and what they changed on the floor. The answer should include specifics—screw RPM, back pressure, nozzle temperature—not just “we adjusted the process.” That level of detail tells you they're reading the material, not just the machine.
Ask to See a Sectioned Casting, Not a Polished Photo
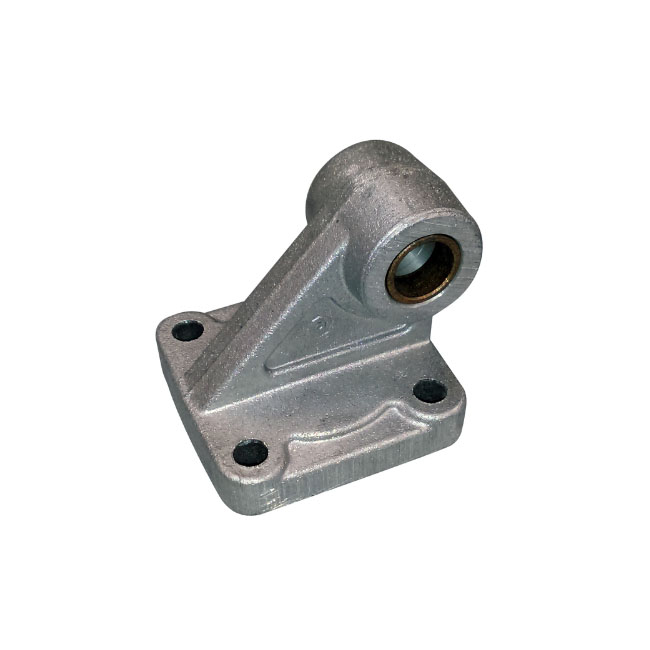
A polished photo can hide a multitude of sins. Surface finishing fills pores, smooths over cold shuts, and makes a mediocre casting look flawless. What you really need to judge is the internal structure — the grain flow, the presence of shrinkage cavities, and the density of the metal where it matters most. That's only visible when the part is cut open.
Insist on a sectioned sample that has been etched or at least rough-cut through a critical load-bearing area. Look for uniform wall thickness, clean transitions between thick and thin sections, and no visible porosity clusters near the surface. If a foundry hesitates to show you a cut section, treat that hesitation as a red flag. It usually means they know what's inside isn't pretty.
Don't settle for a slice from an easily cast test coupon either. Ask for a section taken from the actual production run, ideally from the first cast or a random sample. Compare the cut face against the engineering drawing and check for core shift, cold laps, or off-center cavities. A good foundry will be proud to show you the inside. A bad one will keep handing you glossy photos.
Trace Their Rework and Scrap Rates Over Time
Tracking rework and scrap rates week by week rarely tells a clean story. Early runs often look terrible, then dip as operators learn the quirks of a new part, only to spike again when a supplier change or rushed order shakes the process. Plotting those numbers over time separates random noise from genuine drift.
One useful habit is to overlay rework and scrap on the same timeline. If rework climbs while scrap stays flat, the problem usually sits in assembly or handling, not raw material. When both move together, look upstream—tool wear, batch inconsistencies, or a fixture slowly going out of spec. Monthly averages hide these patterns; daily or shift-level data exposes them.
After a few months of consistent tracking, the rate itself becomes less interesting than its shape. A slow upward creep in scrap often traces back to a dull cutting edge or a filter that hasn’t been changed. A sudden drop usually means someone fixed something quietly—worth documenting before it drifts back.
Throw Them a Design Change and Watch the Response
Introducing a minor tweak to a familiar interface often reveals more about user behavior than any extensive survey. A shifted button, an altered color scheme, or a reordered menu forces people to actively re-engage with the layout. Watch where they hesitate, what they click first, and whether they abandon the task altogether. These small disruptions can uncover hidden assumptions and previously invisible friction points.
The key is to make the change subtle enough that it doesn’t trigger outright confusion, yet significant enough that it can’t be ignored. For example, moving a frequently used action from a prominent spot to a secondary menu might expose how many users rely on visual memory rather than reading labels. The response—ranging from slight pauses to full workaround attempts—tells you whether the original design was truly intuitive or just habitually tolerated.
Run this experiment in a live environment with a small segment of your audience, and compare their completion times and error rates against a control group. Avoid explaining the change beforehand; the goal is to observe raw, unguided reactions. What you learn won’t just validate the current layout—it will give you a sharper instinct for designing changes that users adapt to with minimal frustration.
Confirm Who Performs the Heat Treat and Testing
Pin down exactly which party handles the heat treatment and which one runs the testing. It might sound obvious, but overlaps and gaps happen more often than you'd think when a drawing simply says "heat treat per spec" without naming a responsible group. If the parts go to an outside treater, make sure that vendor also knows whether they're expected to perform hardness checks, tensile pulls, or just the thermal cycle. If testing stays in-house, state clearly which department gets the samples and how they log results back to the job.
A quick phone call or a marked-up traveler beats a long email chain when there's ambiguity. Ask the supplier or your own shop supervisor directly: "Who signs off on the furnace chart? Who cuts the test coupons? Who reviews the certs before they go into the packet?" Write those names or roles into the routing. Don't leave it to the receiving inspector to guess whether the material was already tested or still needs to be sent out. When everyone knows their lane, parts don't sit on a shelf waiting for a test that was never assigned.
If you're working with a new vendor or a revised part number, re-confirm the split of duties even if it's been fine for years. A change in ownership, a new shift supervisor, or a different purchase order format can silently shift the responsibility. Keep a short note in the job file listing who does what for heat treat and testing, and update it whenever the routing changes. That small habit prevents rejected lots, missed certifications, and awkward blame games later.
Check Their Honesty About Porosity and Inclusions
A seller's willingness to discuss porosity and inclusions without hesitation often separates genuine transparency from polished salesmanship. Instead of accepting vague phrases like "minor natural characteristics," ask pointed questions about the size, location, and visibility of any surface-reaching cavities or internal flaws. Watch how they respond: a forthright dealer will pull out a loupe, point to the exact feature, and explain why it doesn't compromise durability. Evasive answers, sudden shifts to color or carat weight, or claims that such details "don't matter for this piece" are red flags that you're being steered away from a material fact you specifically asked about.
Cross-check their narrative against independent evidence. Request a grading report from a recognized laboratory, but don't stop there—ask if they have any in-house magnification videos or high-resolution images taken under different lighting angles. A truly honest vendor will not only provide these but will also flag inclusions that might be missed in a standard report, such as a feather near a prong or a cavity that could trap oil. Compare their verbal description to what you see under 10x magnification. If they claim "eye-clean" and you can spot a black crystal inclusion without effort at arm's length, that's not a difference of opinion; it's a failure of disclosure.
Finally, test their consistency over time. Return to the same stone or set a week later and ask the same questions again. Honest sellers repeat the same details, even the unflattering ones, because those facts are fixed in their records and their memory. Dishonest ones often upgrade the description on the second visit, conveniently forgetting a cavity or downplaying a cloud that you previously noted. Pay attention to how they frame ownership: someone who says "when I bought this parcel, I rejected three pieces because of surface-reaching inclusions" demonstrates a working knowledge of the material, while someone who leans on generic jewelry-store reassurances may never have examined the stone under magnification at all.
FAQ
A vendor worth shortlisting will walk you through their melt shop controls—slag practices, deoxidation steps, temperature checks before tapping, and how they adjust chemistry for thin versus thick sections. If they can't explain why a particular heat treatment cycle was chosen for your grade, they're likely guessing.
Price only matters if parts arrive usable and on time. Ask for on-time-in-full data covering at least the last six months, not just a couple of cherry-picked success stories. A vendor with 95% OTD at a slightly higher quote is usually cheaper by the time you factor in line stoppages and expedited freight.
Ask who signs off on non-destructive testing, whether radiography or ultrasonic testing is done by certified operators, and how they handle borderline indications. You want clear accept/reject criteria tied to ASTM or EN standards, not a vague promise that 'we check everything.'
Look for vendors who use solidification modeling before cutting tooling. A detailed riser and gating layout based on simulation—plus photographs of sectioned sample castings—shows they think ahead. If they rely only on trial and error, your first production run becomes their experiment.
Ask for heat lots tied to actual furnace records and mechanical test samples from separately cast or attached coupons, not just someone's word. Reputable vendors can show traceability from scrap or ingot charge through final heat number. If certs look too clean or repeat numbers month after month, dig deeper.
Watch for vague statements like 'standard casting tolerances apply' without asking about your datum scheme. A serious vendor reviews the drawing and points out where draft, shrinkage allowance, or machining stock may conflict with your design. If they accept everything without a single technical question, they haven't studied the part.
Sector experience helps because failure modes differ: a pump housing may need pressure tightness, while a mining wear part needs abrasion resistance. A vendor with relevant applications will ask about service loads, corrosion, and temperature before quoting. Without that, you may get a structurally sound casting that still fails in your environment.
Agree on reviewable documents before production: casting drawings, weld repair limits, inspection test plans, and acceptance criteria. State clearly who pays for non-conforming parts, rework, or late delivery. The goal isn't to punish the vendor but to make both sides define 'done' the same way on day one.
Conclusion
A foundry's quote rarely tells you how their steel will behave after machining, welding, or a few thousand thermal cycles. Before you commit, ask for the full melt sheet from the last three pours of your alloy family—look at residual aluminum, tramp elements, and nitrogen levels, not just the carbon and manganese they advertise. Then request a sectioned casting from a rejected lot, sawn through the heaviest section. A polished surface hides shrinkage and gas porosity; a cut face reveals whether their risering and gating actually feed the part. Follow that with a year's worth of rework and scrap data, broken down by pattern number. If the rate dips only after a customer complaint, their process control is reactive, not preventive.
Next, throw them a real design change mid-quote—add a boss, tighten a radius, shift a parting line. A capable vendor will redline the drawing, call out solidification risks, and ask about machining stock. A desperate one will accept everything and surprise you later. Ask exactly who performs heat treat, NDT, and mechanical testing. If these are subcontracted, you are buying a broker's promise, not a caster's accountability. Finally, listen to how they talk about porosity and inclusions. A foundry that admits typical defect locations, shows you radiographic indications from past jobs, and explains repair weld limits is one you can plan around. One that claims zero defects without evidence is selling optimism, not castings.
Contact Us
Contact Person: Paul
Email: [email protected]
Tel/WhatsApp: 8615067447509
Website: https://www.spironcasting.com