ODM Mission-Critical Valve Company: Engineering Excellence for High-Stakes Applications
2026-10-22
Most people never think about the valves inside a nuclear plant, an offshore platform, or a high-pressure chemical reactor—until one of them fails. In mission-critical applications, there is no margin for close enough. ZMV has built its ODM reputation on a simple reality: when the stakes are extreme, every component must be engineered as if lives depend on it. Because sometimes, they do.
Where a Leak Could Mean Catastrophe, ODM Valves Hold the Line
In a refinery, a single failing gasket can turn a routine shift into an evacuation. The pipes that carry superheated steam, corrosive acids, or volatile gases don’t forgive shortcuts. That’s where ODM valves earn their keep: each one is built around a metal-to-metal seat and a stem seal that stays tight even after tens of thousands of cycles. The design philosophy isn’t about adding more parts, but about removing the small drifts in tolerance that let a drip become a breach.
Offshore platforms and chemical storage terminals rely on more than just pressure ratings. They need a valve that behaves the same at 3 a.m. as it did on the test bench. ODM’s production line includes helium mass-spectrometer checks on every critical seal, and the castings are X-rayed before machining begins. That kind of scrutiny catches the invisible porosity and micro-cracks that ordinary inspection misses. It’s not about passing a spec sheet; it’s about knowing the flange won’t weep when the tank farm is already at capacity.
A shutdown caused by a leaking valve can cost more than the valve itself a hundred times over, not counting the risk to the crew. ODM valves hold the line because they’re designed for the worst-case scenario, not the average one. When the next isolation point sits between you and a runaway reaction, the margin for error isn’t something you calculate on paper.
Engineering the Last One Percent of Performance
Real speed doesn't come from rewriting the whole stack. It hides in the margins—a cache line fetched too often, a branch mispredicted in a loop that runs a billion times, a buffer sized just slightly wrong. When the obvious wins are gone, the last one percent demands a different kind of patience. You stop looking for big architectural changes and start looking at the shape of data, the order of instructions, the exact moment a lock gets released. Profiling at this level feels less like engineering and more like tuning an instrument by ear.
One thing that consistently matters is removing friction between the hardware and the code. Sometimes that means restructuring a struct so two hot fields don't share a cache line and cause false sharing. Other times it's replacing a generic function with an inlined version that keeps the working set small. These are not glamorous changes. They won't show up in a rewrite announcement or a library update. But when the system is already within reach of its goal, these tiny adjustments are what make the difference between meeting a latency budget and missing it by a handful of microseconds.
It's also worth remembering that the last percent is often invisible to conventional metrics. A 0.8% improvement in throughput might come from moving a log statement out of a tight loop, or from switching a memory allocation to a stack buffer. The work is tedious, and the results rarely feel dramatic in isolation. Yet across enough hot paths, they compound into a system that simply feels faster—responsive in ways that users notice but can't easily quantify.
From First Sketch to Final Torque, a Mission-Critical Valve Takes Shape
The part started as a rough pencil sketch on a coffee-stained notebook page, the kind of idea that gets circled three times before anyone believes it can survive contact with a real flow loop. Our lead engineer spent more time erasing than drawing, chasing a port geometry that would let the poppet close without chatter at 3,000 psi. That early sketch was less a blueprint and more an argument with physics—every line had to justify itself against cavitation, leakage, and the 200,000 cycle requirement buried in the spec.
Once the sketch migrated into CAD, the valve stopped being a sketch and started being a stack of decisions. We swapped the initial 316 stainless body for a duplex alloy after a first-pass FEA showed stress concentrating near the seat under thermal cycling. The prototype machining took eleven setups, and the first two attempts ended up in the scrap bin because the stem runout exceeded 0.0004 inch. That kind of failure doesn't feel like progress until you hold the third part and watch the indicator needle hold steady.
Final torque didn't happen on a test bench in some distant lab; it happened on the assembly floor, with a calibrated wrench and a witness marking the bolt heads. The spec called for 47 newton-meters, but the real acceptance test was the leak-down after 500 hot cycles with helium. When the last bubble never formed, the valve earned its install. It's not the sketch that matters in the end, or even the torque—it's the fact that the line it protects will run unattended for the next six years.
Not All Valves Are Built for This
A quick glance at two ball valves might suggest they're interchangeable, but the similarities end at the outer shell. Seat materials, stem seals, and body alloys are chosen for specific fluids, pressures, and temperature swings. Put a brass water valve on a hot glycol line or a chemical dosing loop and the seals can swell, crack, or wash out within weeks.
Even valves that share the same nominal size and connection type often follow different testing and certification paths. One might be fine for low-pressure compressed air, while another is built to handle saturated steam or abrasive slurries. Those differences rarely show up in a catalog photo, but they become obvious once the valve is asked to do something it was never designed to do.
The real cost of using the wrong valve is rarely the purchase price—it's the downtime, leaks, and safety risks that appear later. Matching the valve to the actual service conditions, including cycling frequency and possible pressure spikes, matters far more than matching the pipe size.
The Testing Regimen That Rejects Anything Less Than Perfect
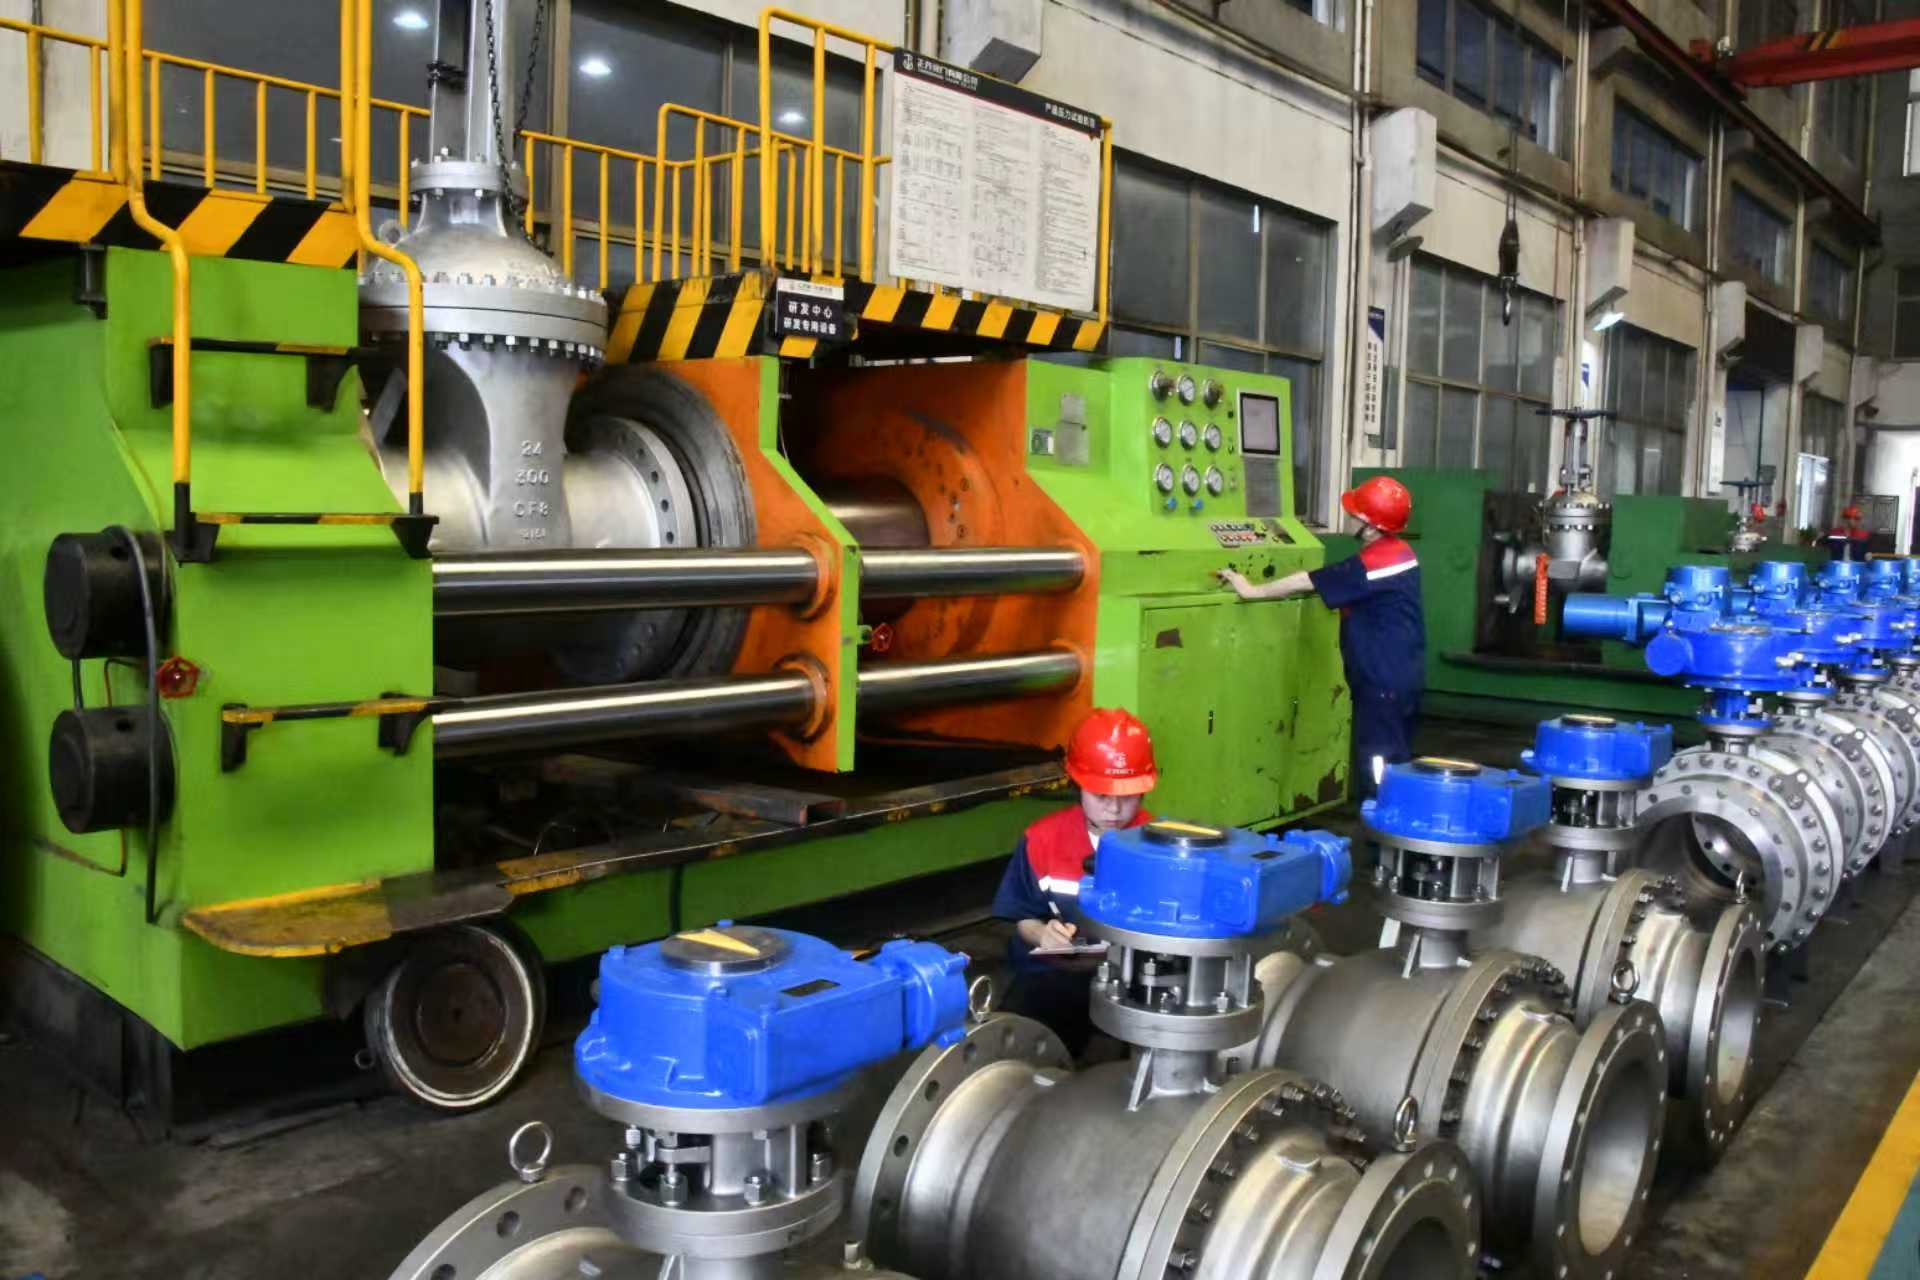
Every product that leaves the facility must survive a gauntlet where tolerance for imperfection is zero. The testing regimen isn't a polite checklist; it's an uncompromising filter that treats 'good enough' as a failure mode. Each unit endures stress cycles, environmental extremes, and precision measurements that expose even fractional deviations from spec. There is no passing grade below flawless.
What sets this process apart is its refusal to negotiate with mediocrity. A single micro-fracture, a drift of two microns, or a temperature variance outside a narrow band triggers rejection and a full root-cause investigation. The goal isn't to catch most defects—it's to make any defect statistically impossible. This philosophy drives the lab's instrumentation choices, sampling rates, and the brutal reality that a batch is only as strong as its weakest sample.
The result is a benchmark that competitors quietly study but rarely copy, because the cost of such rigor is high. Yet for those who demand components that work under conditions where failure is not an option, this regimen isn't excessive—it's the only honest definition of quality. Anything less than perfect is simply not allowed to wear the name.
The Quiet Backbone of High-Stakes Operations
In every high-stakes operation—whether a surgical team navigating a complex procedure, a flight crew managing an in-flight emergency, or a financial desk holding positions through volatile markets—there exists a layer of work that rarely gets named. It is not the loud decision or the visible maneuver. It is the constant, low-frequency hum of coordination: the unspoken checks, the quiet logging of parameters, the second pair of eyes that scans without being asked. This layer often goes unnoticed precisely because it functions so smoothly. Yet when it falters, the entire operation tilts.
Consider the individuals who monitor instrument panels for hours without a single abnormal reading, who cross-reference checklists not because a rule demands it but because the habit has become second nature. Their value is not in dramatic intervention but in the prevention of drama altogether. They are the ones who notice a subtle drift in a metric long before it becomes a threshold breach, who adjust a schedule or re-route a resource without fanfare. In high-pressure environments, attention is currency—and these quiet operators spend it with relentless discipline, never needing recognition to keep the machinery aligned.
What makes this backbone truly quiet is not silence, but a deliberate rejection of self-importance. The work does not seek a spotlight; it seeks reliability. Teams that last in high-stakes fields tend to cultivate this ethos: praise is redirected, credit is diffused, and the focus remains on the next small thing that could go wrong. It is a form of operational humility—knowing that the most critical contribution might be the one nobody remembers, because everything simply worked as it should.
FAQ
We start by mapping every stress point, pressure cycle, and corrosion vector the valve will face over its service life. Instead of relying on off-the-shelf geometries, our engineers modify seat angles, stem sealing, and body wall thickness based on the actual operating envelope. Prototypes then go through accelerated life testing that replicates years of thermal cycling and particulate erosion in weeks.
The list includes offshore production platforms, subsea wellheads, refinery emergency shutdown systems, chemical injection skids, and high-pressure gas storage. We also support specialized defense and aerospace ground support equipment where documentation and traceability are non-negotiable.
Yes, we routinely machine valve bodies and trims from duplex stainless, Inconel, Monel, and titanium. Our in-house heat treating and cryogenic processing allow us to tune material properties for services from minus 320°F to over 1,200°F without outsourcing critical steps.
Every valve is serialized and tracked from raw material heat number to final assembly. We perform hydrostatic shell tests, pneumatic seat leakage tests, and helium mass spectrometer testing on request. For critical orders, a dedicated quality engineer signs off on each dimensional report and NDT result before the valve ships.
Depending on the complexity, we can move from concept to first article in eight to fourteen weeks. We keep a library of pre-qualified trim designs and body patterns that can be adapted quickly, which avoids the months-long design cycle many larger manufacturers require.
We offer field service teams that can perform in-situ lapping, seat replacement, and actuator calibration without removing the valve from the line. We also maintain a digital twin of every critical valve we ship, so if a client calls with a serial number, we can pull up the exact material certs, torque settings, and service history in minutes.
Many commodity valves are engineered to a price point, not a performance envelope. Clients come to us after seal washouts, stem galling, or body erosion caused by underestimated flow velocities. We re-engineer the valve around the actual fluid dynamics and then validate the fix with computational flow modeling and real-world flow loop testing.
Conclusion
In environments where a single leak can trigger catastrophic failure, ODM valves do more than open and close—they hold the line. The company does not chase broad product lines or generic certifications. Instead, it focuses on the last one percent of performance that separates a dependable component from a liability. Every ODM valve is built from the ground up with the understanding that not all valves are engineered for this kind of pressure, temperature cycling, or corrosive exposure. The result is hardware that operators trust when there is no room for error.
That trust is earned long before installation. A mission-critical valve at ODM takes shape through a deliberate path from first sketch to final torque, with every material choice and machining step tied to the demands of high-stakes service. Nothing leaves the facility without passing a testing regimen designed to reject anything less than perfect—because a borderline part is not an acceptable risk. This is why ODM has become the quiet backbone of operations where failure is not an option, supporting critical infrastructure without demanding attention until the moment it matters most.
Contact Us
Contact Person: Lucas Lin
Email: [email protected]
Tel/WhatsApp: +8613968913000 / +8613868610141
Website: https://www.zhengmaogroup.com