High-speed Wire Rod Mill Solutions for Maximum Production Efficiency
2026-10-05
In the competitive world of wire rod production, every second of downtime and every millimeter of tolerance deviation cuts into your bottom line. High-speed wire rod mills are the backbone of modern steel processing, yet not all solutions deliver the speed, precision, and reliability that high-output operations demand. That’s where GRM steps in—redefining what maximum production efficiency truly means. From breakthrough rolling speeds to intelligent automation and wear-resistant designs, GRM’s high-speed wire rod mill solutions are engineered for mills that refuse to settle for average. Whether you’re chasing higher tonnage, tighter tolerances, or longer roll life, this guide unpacks the key technologies and strategies that can turn your production line into a benchmark for the industry.
Precision Rolling That Cuts Seconds, Not Corners
Every run starts with a clean line and ends with a finish that feels almost unfair. Our precision rolling doesn't just shave time—it rewrites how you read the terrain. The weight distribution stays so neutral through transitions that your muscle memory starts trusting the board more than your eyes.
What separates a good setup from a great one is how little you notice it working. We tune the flex pattern and edge bevel to match your stance width and riding style, so the board responds before you finish the thought. No chatter, no fighting for grip, just smooth acceleration out of every turn.
The result is a ride that carries speed through flat sections and holds tight on icy traverses without forcing you into a rigid pose. You stop counting seconds and start linking turns that feel preordained. That's the difference between rolling fast and rolling right.
Thermomechanical Control for Consistent Wire Properties
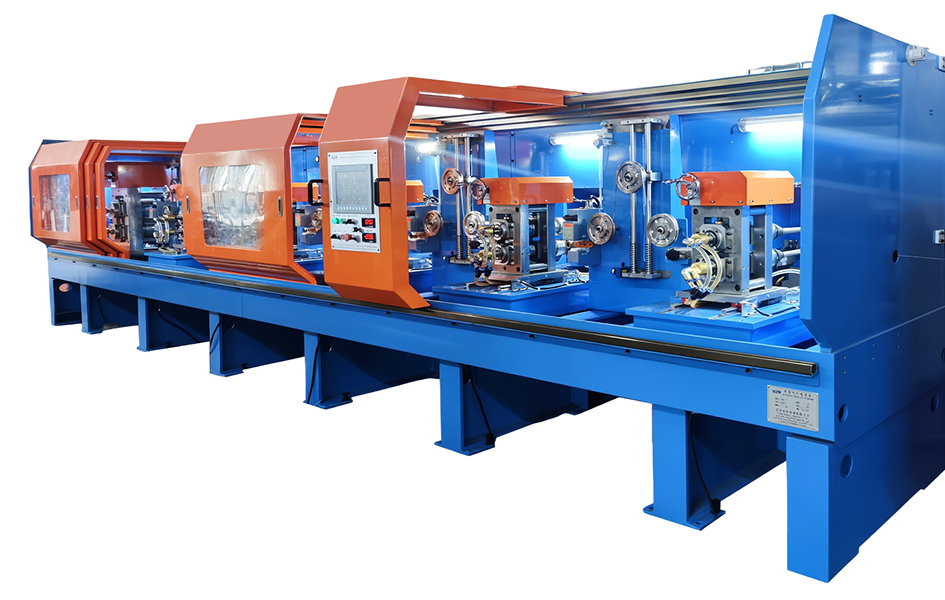
Achieving repeatable mechanical and electrical behavior in drawn wire hinges on managing the interplay between deformation heat and the cooling path. The goal is not simply to hit a target diameter, but to keep the accumulated strain, dynamic recovery, and recrystallization within narrow bands. When finishing passes run too hot, grain growth softens the wire and raises elongation unpredictably; when quenching is too aggressive, locked-in stresses can create springback and off-spec tensile values. A tight thermomechanical window therefore pairs pass reduction with roll or die temperature, emulsion flow, and take-up tension so that each spool leaves the line under nearly identical thermal history.
In practice, operators adjust coolant pressure and inlet temperature against measured wire surface temperature at multiple points along the strand. Small shifts in emulsion concentration or nozzle alignment can change heat extraction enough to move the final tensile strength by several percent. For alloys prone to age softening or precipitation, hold times between passes and coiling temperature matter as much as the drawing itself. Capturing these variables in a live process model allows the line to compensate for incoming rod hardness, tool wear, and ambient swings instead of relying on downstream sorting.
The payoff shows up as fewer breaks during stranding and more uniform elongation in finished conductors. Instead of chasing property drift with lubricant tweaks or capstan speed changes after the fact, the line keeps the wire within a controlled thermal and strain corridor from entry to spool. That consistency reduces scrap, simplifies certification testing, and gives downstream forming or insulation processes a more predictable starting material.
Automated Tension Management Across Every Stand
Tension drift between stands rarely announces itself — it shows up as edge curl, uneven coating, or a sudden spike in motor load. Instead of waiting for an operator to catch the trend, the system reads strip speed, roll force, and dancer position every few milliseconds and nudges the drive references before a small deviation becomes a visible defect.
Each stand gets its own closed-loop target, but they share a common model of what the line is doing further upstream and downstream. This keeps a correction at stand three from over-tightening stand four, which is the usual failure point for fixed per-stand PID tuning. The result is less manual intervention, fewer rejected coils, and speed changes that don't ripple through the line as tension shocks.
Energy Recovery Systems That Lower Cost Per Ton
Instead of letting exhaust heat or pressure bleed away, plants can route that wasted energy back into the production cycle. A well-placed recovery unit captures thermal discharge from dryers, kilns, or compressors and feeds it into preheating, steam generation, or facility climate control. The result is a direct drop in fuel consumption per processed ton, often visible within the first few billing cycles.
Beyond fuel savings, these systems reduce the load on primary equipment. When recovered energy handles a portion of the heating demand, boilers and furnaces run fewer hours at peak output, which cuts maintenance intervals and extends asset life. In high-volume operations, that reliability gain translates into fewer unplanned stoppages and a steadier throughput rate.
The economics improve further when recovery is paired with variable-speed controls and smart routing. Instead of operating at a fixed recovery rate, the system adjusts to real-time demand, avoiding waste during low-production windows. This keeps cost per ton low across a range of output levels, not just at full capacity.
Predictive Maintenance Without Production Interruptions
Keep machines running while watching for early signs of trouble. Vibration sensors mounted on rotating parts, thermal cameras tracking heat buildup, and acoustic detectors listening for bearing wear all feed data into a live model that learns what normal looks like for each asset. When the pattern drifts, the system flags a specific component and estimates how many operating hours remain before failure—no shutdown required for inspection.
The trick is moving analysis to the edge. Instead of shipping raw sensor streams to a central server, small industrial PCs next to the equipment run lightweight models that only send alerts when something changes. This cuts bandwidth costs and lets the maintenance team act on a Tuesday afternoon rather than waiting for the next scheduled outage. Spare parts can be ordered and a repair window squeezed into a shift change or a brief line slowdown.
Some plants pair this with digital twin simulations. The real machine's sensor data updates a virtual copy, which then runs accelerated wear scenarios to predict when a pump seal or gearbox bearing will cross its safe threshold. Because the twin lives in software, you can test different operating loads or lubrication schedules without touching the physical asset. That means the production line never stops just to find out if it's still healthy.
From Billet to Coil: Streamlined Handling for Faster Turnaround
Moving steel from its raw billet form into finished coil used to involve multiple handoffs, waiting periods, and unnecessary crane movements. By rethinking the flow, we eliminated those bottlenecks—billets now travel through a continuous sequence where heating, rolling, and coiling happen with minimal interruption. The result isn't just a faster line; it's a predictable one, where every piece arrives at the next station exactly when it should.
The key change came from coordinating the handling equipment itself. Instead of treating each crane or transfer car as an independent step, we synchronized their paths so that a billet is picked up once and carried through several stages without being set down and re-gripped. This cut transfer time nearly in half and reduced surface damage that used to come from repeated clamping. Operators now see fewer alarms, fewer manual interventions, and more consistent coil weights.
Faster turnaround doesn't have to mean rushing. It means removing the empty motion that adds no value. With streamlined handling from billet to coil, we've trimmed hours from each production cycle, lowered energy use, and given downstream processes a steadier supply of material. That's the kind of efficiency customers notice on their delivery schedule.
FAQ
A high-speed mill uses a no-twist finishing block, tighter roll pass sequences, and faster delivery speeds typically above 100 m/s. This setup delivers tighter dimensional tolerances, better surface finish, and more consistent mechanical properties compared to older open-train mills.
Efficiency comes from reducing cobble rates, shortening guide and roll change times, and maintaining steady tension between stands. Pairing these practices with in-line gauging and closed-loop speed control keeps both output and quality high.
Common grades include low-carbon wire for drawing, high-carbon wire for springs and ropes, cold heading quality steels, and bearing steels. Each grade requires a specific cooling path to meet the desired tensile strength and ductility.
Automation monitors rolling force, loop height, and temperature in real time. It adjusts roll gaps and stand speeds automatically, which prevents operator delay and reduces dimensional variation during acceleration and deceleration.
Water boxes and the laying head temperature control the transformation of austenite. With precise cooling, the mill can run faster because the wire reaches the required microstructure without waiting for slow air cooling, and the final tensile strength stays within specification.
Frequent inspection of roll rings, guides, and oil-film bearings is essential. Vibration trending, regular lubrication checks, and scheduled replacement of wear parts before failure prevent unplanned downtime and keep the mill at full speed longer.
Yes. Retrofitting a no-twist finishing block, adding higher-capacity drives, installing loop scanners, and upgrading the cooling conveyor can significantly raise rolling speed and product consistency without building a new line.
The main risks are front-end cobbles, tension overload between stands, and accelerated roll surface wear. These are managed through precise guide alignment, automatic tension control, and real-time torque monitoring that slows the mill instantly when abnormal conditions appear.
Conclusion
Achieving maximum output from a high-speed wire rod mill depends on how well each stage respects both speed and material integrity. The rolling sequence uses precision passes that remove only the necessary time from inter-stand gaps, keeping dimensions tight while pushing throughput upward. Rather than relying on post-rolling corrections, thermomechanical control works inside the process window to lock in uniform grain structure and tensile properties across every coil. Automated tension loops between stands continuously trim speed differentials, so the stock never surges or stretches, which is often where hidden cobbles and dimensional drift begin. These systems work together to make higher rolling speeds feel less rushed and more deliberate.
On the cost side, energy recovery captures braking and exhaust heat that would otherwise leave the line, feeding it back into preheating or auxiliary drives to reduce expense per ton. Predictive maintenance watches torque signatures and bearing temperatures without stopping production, allowing roll changes and guide adjustments to happen during planned pauses rather than after a failure. Finally, moving billets to coils with fewer transfer points shortens turnaround, while automated coil handling keeps the hot product moving toward the next process instead of sitting in a queue. These combined measures let a mill sustain higher utilization without adding crew or floor space, which is the real meaning of production efficiency in a high-speed wire rod operation.
Contact Us
Contact Person: Rayna
Email: [email protected]
Tel/WhatsApp: 86 -173 1474 6343
Website: https://www.grmrollingmill.com/