Advanced Corrugated Box Die Making Creasing Cutting Machine Boosts Packaging Output and Precision
2026-09-27
Packaging demand keeps climbing, and corrugated box makers are feeling the pressure to produce more without sacrificing quality. That’s where an advanced die making creasing cutting machine changes the game—turning tight deadlines into manageable output and rough edges into repeatable precision. For teams ready to move beyond outdated equipment, ADEWO offers a practical path forward. This article breaks down the key ways modern creasing and cutting technology can raise both throughput and accuracy on your packaging line.
Why Precision Creasing Shows Up in Faster Box Assembly
When a box blank comes off the die-cutter with crisp, consistent crease lines, the folding step practically runs itself. Operators aren't stopping to wrestle with panels that drift or pivot at the wrong point. That's the hidden cost of sloppy creasing: every misfold steals seconds, and those seconds stack up across a full run. Precision creasing removes that friction before it starts.
It's not just about speed on the line. A clean crease makes the board's memory work in your favor. The fibers are guided to fold exactly where intended, so the flap snaps into place rather than being forced. That means less dwell time in the folding section, fewer jam-ups, and far less need for manual rework at the delivery end. When the geometry is predictable, the whole assembly sequence tightens up.
There's also a knock-on effect with glue and tape application. If panels meet perfectly, adhesive bonds form on the first pass. If they're off by a millimeter, you're adding compression time or scrapping boxes altogether. Precision creasing keeps tolerances tight enough that high-speed lines can actually run at their rated capacity instead of crawling along to compensate for variation.
Cutting Through Corrugated Without Sacrificing Edge Quality
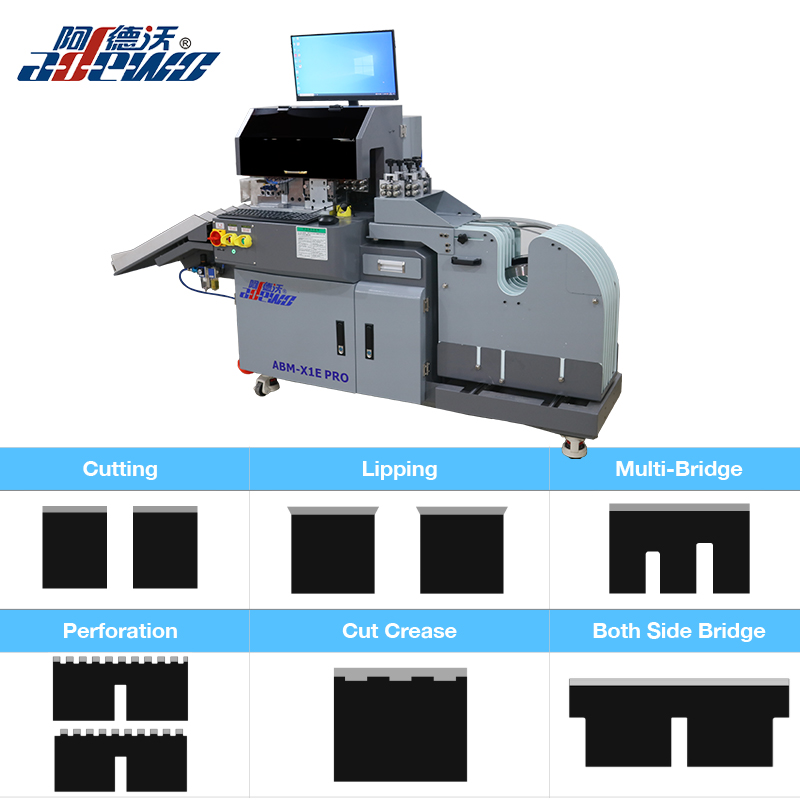
Corrugated board has a habit of fighting back—those fluted layers vibrate, compress, and tear if the blade geometry isn’t matched to the material’s density. The usual fix of slowing the feed rate or forcing a heavier downcut only swaps one problem for another: fuzzy edges, crushed flutes, or delamination near the cut line. A sharper approach pairs a shallow cutting angle with controlled oscillation so the blade slices through the medium without dragging debris through the kerf.
Edge quality hinges on how well the tool handles the paper liners and the fluted core at the same moment. When the tip enters too steeply, the top liner can deflect before it’s cleanly severed, leaving a ragged lip that shows up on the finished box. Keeping the blade’s bevel shallow and its stroke short reduces that deflection and lets the flutes collapse inward rather than outward, which preserves a crisp, square edge even on double-wall stock.
The real test comes on long production runs, where adhesive residue and paper dust build up on the cutting edge. Instead of reaching for a faster blade speed, which overheats the tip and accelerates wear, run a dry lubrication routine and monitor the edge under magnification. A dull edge doesn’t just cut poorly—it changes the way the board separates, so catching micro-chipping early keeps the cut clean without slowing the line down.
What Advanced Die Making Changes for Custom Box Turnaround
For years, custom box production was held back by the slow, hands-on process of crafting steel rule dies. Each new shape or size meant measuring, bending, and welding by hand—a bottleneck that could stretch lead times to weeks. Advanced die making turns that on its head. Laser-cut dies, CNC routing, and digital templates now allow a die to be produced in hours, not days. This shift means a custom box project can move from approved artwork to a finished die in a single day, compressing the entire turnaround drastically.
The real difference comes from precision and repeatability. Traditional dies often needed multiple test cuts and adjustments before they produced clean scores and cuts. Modern methods like automated bending and 3D-printed stripping units eliminate much of that trial and error. With a die that works correctly on the first press run, there’s no back-and-forth between die maker and printer. Box manufacturers can take on short-run custom orders with confidence, knowing the tooling won't slow down delivery.
Digital file transfer also plays a role. A customer’s dieline can be converted directly into machine instructions, removing manual interpretation. This seamless handoff between design and production means even complex packaging with multiple cutouts or unique tuck flaps can be tooled quickly. What used to require a specialist with years of experience now moves through a streamlined, software-driven process, trimming days off the schedule without sacrificing quality.
Automating the Repetitive Parts of Box Production
Box production often involves countless repetitive steps that slow down the entire line. From folding flaps to applying adhesive, these tasks are usually done by hand or with outdated machinery. Automating them can cut cycle times dramatically. Instead of relying on workers to repeat the same motion every few seconds, smart sensors and programmable arms handle the work with consistent speed. This frees up your team for more complex jobs like quality inspection or custom packaging design.
One of the biggest advantages of automation here is repeatability. A machine doesn't get tired or lose focus after a long shift. It applies the same pressure, the same tape length, and the same fold angle every single time. That level of consistency reduces waste caused by human error. Boxes come out uniform, which means fewer rejects and less material thrown away. Over time, those savings add up in both raw materials and labor hours.
Implementing automation doesn't have to mean a full factory overhaul. Start with the most tedious bottleneck, like corner cutting or pallet strapping. Retrofit existing equipment with smart controllers or add a dedicated cell that handles only that task. Many smaller systems pay for themselves within months through higher throughput and lower error rates. The goal is to keep the creative, judgment-heavy parts of box production in human hands while letting machines own the repetitive grind.
The Hidden Costs of Inaccurate Creasing and How to Avoid Them
The real problem with inaccurate creasing rarely shows up at the creasing machine. It appears later, at the folder-gluer or in the customer's hands, when cartons refuse to fold cleanly or the paper cracks along the spine. A single misjudged crease depth can turn a standard run into a manual rework nightmare—operators slowing down to fix bad folds, stacks set aside for inspection, and deadlines slipping. Those hidden labour hours and lost machine capacity often cost far more than the wasted sheets themselves.
Avoiding this starts with treating creasing as material-specific, not one-size-fits-all. Paper weight, grain direction, and coating all change how the fibre responds under pressure. A quick strip test on the actual stock beats trusting the settings from the last job. Adjust the crease rule depth and width until the fold feels firm but the surface shows no signs of cracking or whitening. Also check the counter plate and creasing matrix for wear—damaged tooling quietly ruins consistency even when the machine settings look right.
Beyond setup, build regular checks into the run. Pull samples every few hundred sheets and fold them the same way the end user will. If you notice slight fibre lift or uneven resistance, stop and recalibrate rather than pushing through. A few minutes at the creaser prevents hours of hand-folding rejects and protects the reputation that brings repeat orders. In short, accurate creasing is less about perfect machines and more about paying attention before small errors compound into visible, costly defects.
Long-Run Consistency Without Constant Adjustments
Achieving long-run consistency rarely comes from constantly tweaking every variable. More often, it emerges when the core principles are sound enough to survive minor fluctuations. Think of a well-designed thermostat: it doesn't need manual adjustment every few minutes because the underlying feedback loop already handles small temperature shifts. In the same way, a personal habit, an investment strategy, or a production process becomes reliable when its foundation is robust, not when someone is endlessly fine-tuning the edges.
The urge to adjust constantly often stems from a misunderstanding of what consistency actually requires. We assume that if we aren't actively modifying something, we're falling behind. Yet constant adjustments can introduce noise, reduce predictability, and wear down the people or systems involved. A fitness routine that changes every week never lets the body adapt to a stable stimulus. A pricing model that shifts with every market rumor erodes customer trust. True consistency is less about reacting to every short-term signal and more about trusting a structure that has been designed to absorb ordinary variation.
This doesn't mean ignoring real problems or refusing to improve. It means distinguishing between noise and genuine drift. When a process is aligned with a clear, long-term goal, occasional deviations tend to self-correct without panic. The gardener who waters deeply and mulches properly doesn't rush out to adjust the soil every sunny afternoon. The writer who has built a daily drafting rhythm doesn't rewrite the outline each morning. Long-run consistency is a byproduct of getting the fundamentals right and then having the discipline to leave them alone long enough to work.
FAQ
It combines precision creasing and cutting in one smooth operation, which reduces manual adjustments and keeps board feeding consistent. Operators notice fewer jams and sharper fold lines even at higher speeds.
The automated feeding and quick-change die system let you run longer batches without stopping for recalibration. Many plants see daily throughput rise by twenty to thirty percent once the settings are dialed in.
Yes, it adjusts automatically to single, double, and triple wall boards within a wide caliper range. The pressure control reacts to board density, so you don't have to reset parameters for every job.
Clean, consistent creases mean the box folds squarely and the joints align without bulging. That reduces rejected blanks and makes the finished cartons stack and palletize more neatly.
Daily upkeep is mostly limited to lubricating a few accessible points and clearing dust from the sensors. The touchscreen interface uses plain language and stores job recipes, so new operators can learn the basics within a couple of shifts.
The cutting unit uses a hardened steel rule and servo-driven pressure, which gives a clean edge with minimal fiber tear. Because the blade movement follows the same path every cycle, slot depths and panel widths stay within a tight tolerance.
High-volume corrugated converters, e-commerce packaging suppliers, and just-in-time box plants get the biggest advantage. It's especially useful when orders change frequently and you need fast changeovers without sacrificing repeatability.
Yes, the servo motors draw power only when the ram is cycling, and the precise blank alignment cuts down on wasted board from mis-set scores. Over a year, that can add up to a meaningful reduction in both electricity and corrugated sheet waste.
Conclusion
On the floor of a busy corrugated box plant, the difference between hitting a delivery date and falling behind often comes down to how cleanly the creases land and how true the cuts run. The advanced creasing and cutting machine changes that equation. By pairing rigid die-making precision with tight control over pressure and depth, it lets boxes fold flat without fighting the board, so assembly crews move faster and fewer units get rejected for skewed panels or crushed fluting. Edge quality no longer depends on blade wear checks every few hours; the cutting station maintains a consistent shear through double-wall and heavy-duty grades, leaving edges crisp enough for retail-ready print and strong enough to survive rough handling.
For custom work, the shift is just as noticeable. Die changes that once tied up a machine for half a shift now happen in minutes, and the repeatability means the last box off a long run matches the first. This removes the usual gamble of adjusting crease depth mid-order and throwing away warped or torn blanks. Automating repetitive steps—loading dies, setting nip pressures, tracking the wear on creasing rules—frees operators to watch the line instead of babysitting dials. The hidden costs of inconsistent creasing show up as slow folding, popped joints, and compressed edges that weaken stacking strength; by holding crease placement to a tight tolerance, the machine avoids those quietly expensive failures. The result is a line that runs longer between adjustments and still turns out packaging that fits, protects, and stacks the way it should.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com