3-in-1 Filling Machine Solution for Streamlined Packaging Efficiency
2026-10-22
Packaging lines rarely grind to a halt for a single dramatic reason—they lose speed in the small gaps between washing, filling, and capping. A 3-in-1 filling machine solution closes those gaps, but the real test is how well it adapts to your containers and production rhythm. Here’s how Wanying Machinery turns that integrated approach into streamlined packaging efficiency without forcing your line into a rigid template.
One Machine, Three Jobs: The Logic Behind Consolidation
Walk into a professional kitchen and you’ll see a single piece of equipment that can steam, bake, and roast. In a manufacturing plant, one machine might cut, drill, and tap a metal part without moving it between stations. The idea isn’t new, but the urgency behind it has grown: fewer machines mean less floor space, less power drawn, and fewer operators to train. When you consolidate three jobs into one frame, you stop paying for idle capacity in two other machines while the first one runs.
The logic goes deeper than cost savings. Every time a workpiece or a batch of ingredients moves from one dedicated tool to another, you introduce waiting, alignment errors, and contamination risk. A combined unit eliminates those handoffs by keeping the process inside a single chamber or spindle. Designers also discover that the constraints of one function can improve another — the cooling channels for a milling head, for instance, might naturally distribute heat for an integrated hardening step. That kind of cross-optimization rarely happens when each job has its own box on the floor.
Of course, consolidation has its limits. A machine that tries to do everything often does nothing well, so the real skill lies in choosing which three jobs belong together. The best examples come from observing actual work sequences: if a part is always drilled after it’s turned, combining those steps into one setup removes a fixture and a tolerance stack-up. The point isn’t to shrink the tool count for its own sake. It’s to match the machine’s capabilities to the natural rhythm of the work, so the machine itself becomes a quiet argument against unnecessary motion.
Speed and Floor Space: What Actually Changes on the Line
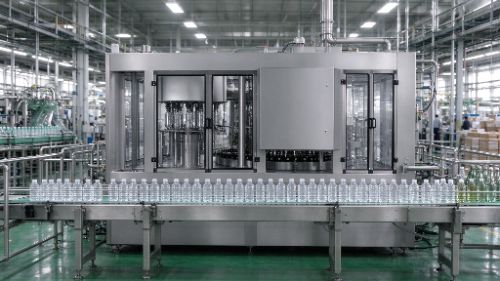
Line speed changes rarely stay at the conveyor. When output per hour climbs, the strip of floor between stations begins to shift: raw material staging creeps closer to the first operation, while finished goods queue in space that used to hold empty pallets. A line that once breathed with open aisles can suddenly feel pinched, not because the building shrank, but because the rhythm of material movement changed.
Buffers are where the trade-off becomes visible. A faster line needs enough work-in-process queued between steps to absorb small stoppages, yet every buffer adds square footage that cannot be used for value-adding work. Sometimes running slightly below maximum speed shrinks the buffer requirement enough to reclaim a full lane of floor space, which then allows easier forklift turns or a second inspection table.
The less obvious changes happen at the margins: tool carts get relocated, maintenance walkways narrow, and operators lose the elbow room that prevents fatigue. If speed increases without adjusting these edge zones, the line can technically run faster while losing more time to blocked exits and restocking trips. Smart layouts respond by going vertical with component racks or shifting subassembly offline, keeping the main line compact without asking people to work shoulder to shoulder.
Quick Changeovers That Keep Short Runs Profitable
Setup time eats margin fast when runs are short. A press brake or CNC lathe idled for 45 minutes between 20-minute jobs can't earn back the lost capacity. Quick changeover work starts with separating internal tasks from external tasks, so everything from tooling to programs is staged while the previous job is still running.
Visual cues and standardized locations take the guesswork out of the next setup. Dedicated carts with pre-measured fixtures, preset offsets, and inspection gauges mean operators aren't hunting for shims or chasing down a forklift. Some shops cut changeovers further by assigning two people for five focused minutes instead of one person wandering for twenty.
Short runs stay profitable when changeover time is treated like machine time—measured, tracked, and challenged. A simple log of what actually stopped the spindle during setup often reveals recurring delays like missing collets or unclear work instructions. Fixing those small, repeated interruptions tends to deliver more margin improvement than speeding up the cutting cycle itself.
Precision Fill Levels Without Rework or Giveaway
High-speed filling lines often hide small giveaways in plain sight—an extra few milliliters per bottle, a slightly overfilled pouch, a can topped off 'just to be safe.' Those fractions add up fast, eating into margin without any customer benefit. Precision fill levels replace that guesswork with real-time measurement and instant correction. Whether it's a load cell under the fill head or an in-line magnetic flow meter, the system reads actual dispensed volume and adjusts the valve closure in milliseconds. The target stays tight, not padded.
More importantly, this accuracy isn't achieved by slowing the line or adding manual inspection steps. Fill algorithms learn from each cycle, compensating for viscosity shifts, temperature drift, or nozzle drip before those variables cause underfills or overfills. A container that falls outside tolerance is flagged immediately and diverted, so nothing reaches the customer short-filled. Rework becomes the exception rather than the routine. Meanwhile, giveaway drops to a statistical rounding error, which means you ship exactly what you intend—no more, no less.
Operators notice the difference on the floor. There's no constant fiddling with fill height settings, no end-of-shift rechecking of dozens of containers, and no pile of 'reject but maybe usable' product waiting for a decision. The equipment holds its calibration across batches and shift changes. When a new product or container size comes in, the changeover is a recipe update, not a trial-and-error session. That reliability frees up time and mental bandwidth for the tasks that actually need human judgment.
Handling Thin Liquids to Thick Pastes with the Same Setup
Many production lines have to switch between watery sauces and heavy pastes without changing equipment. The key is a system that relies on gentle displacement rather than aggressive shear. A progressive cavity pump with a flexible stator can handle both extremes because the seal line continuously adjusts to the material's viscosity. You simply set the speed and let the pump's geometry do the work, whether it's moving a thin brine or a dense tomato concentrate.
The real trick is avoiding air entrapment when moving from one consistency to another. A hopper with a wide throat and a powered auger feed works for thick pastes, while a simple gravity feed suffices for thin liquids. Use a variable frequency drive to fine-tune the flow rate on the fly. No need to swap rotors or stators for most food-grade applications—just flush with warm water between batches to prevent cross-contamination and keep the setup ready for the next product.
What often gets overlooked is the suction piping. For thin liquids, a larger diameter pipe prevents cavitation; for pastes, a shorter, steeper inlet reduces shear and keeps the product from bridging. By matching the inlet design to the most challenging material—the thick paste—you automatically cover the thin liquids. One setup, minimal adjustments, and the line keeps moving.
Service Points Placed Where Operators Can Reach Them
On the production floor, a grease fitting tucked behind a guard panel might as well not exist. Operators rarely have time to hunt for hidden lubrication points, so the best designs bring service ports out to the front edge of the machine, right at hip or shoulder height. This keeps routine checks quick and reduces the temptation to skip them.
The placement logic goes beyond convenience. When a filter, drain valve, or test point sits within arm's reach from the main walkway, maintenance becomes a ten-second task instead of a ladder-and-flashlight expedition. It also cuts the chance of accidental damage to nearby wiring or tubing because nobody has to thread an arm through a narrow access hole.
We treat reachability as a hard requirement during layout reviews. Each service point gets mapped against the operator's normal stance and hand clearance, and anything that fails the reach test is moved or given a remote extension. The result is a line where daily upkeep happens without special tools, awkward postures, or production delays.
FAQ
It merges bottle rinsing, product filling, and cap tightening into one compact frame. Instead of running three separate stations with conveyors between them, operators load containers at one end and get finished, capped bottles at the other.
Most lines see a 20–35% throughput increase simply because there are no transfer gaps or waiting zones between machines. The integrated star-wheel transport keeps containers positively controlled from rinsing to capping, so you can run at speeds closer to the filler's maximum rating.
It works well for beverages, dairy, sauces, personal care liquids, and light chemicals. Any product that needs a clean container, accurate fill volume, and secure cap without manual handling fits the design. Viscous products like honey or shampoo can also run if the filling valves are sized correctly.
No, most adjustments are tool-free. The guide rails, star wheels, and capping head height are set with hand knobs or digital recipe recall. A well-trained operator can complete a format change in 15–30 minutes depending on the number of change parts.
Daily tasks are mainly visual checks and wipe-downs: inspect fill nozzles for drips, clear any broken glass or plastic from the star wheels, and verify the cap chute is free of jams. Weekly, you should grease the main cam followers, check belt tension, and run a no-container test cycle to confirm sensors are aligned.
Yes, within limits. Thin liquids use standard gravity or pressure filling valves, while thicker products need piston or pump-fed valves. Changing product type usually requires swapping the filling nozzles and possibly the hopper, but the frame, transport, and capping station stay the same.
Because the container is held in a positive grip from rinse to cap, there is no tipping or misalignment between stations. Fill accuracy improves by roughly 0.5–1% because the container is perfectly centered under the nozzle every time. Drips and spills drop into a central drain pan rather than onto a conveyor, making cleanup faster and cutting product loss.
You can choose the number of fill heads, the capping type (screw, snap, press-on), the rinsing medium (air, water, or sanitizing solution), and the frame material for corrosive environments. Some builders also offer servo-driven capping torque control, integrated checkweighers, and data logging for batch traceability.
Conclusion
A 3-in-1 filling machine changes how a packaging line is arranged because it combines three separate operations into a single, compact frame. Instead of linking a filler, a capper, and a plugger through conveyors and sensors, operators work with one transfer point and one control interface. The immediate effect is less floor space consumed and fewer places where a container can jam or fall. Speed gains do not come from running the filler faster alone; they come from removing the small delays that accumulate between standalone machines. When a short run switches from one product to another, the changeover is handled with quick-release guides and a limited set of size parts, so the line can return to production without lengthy downtime. This is especially useful for co-packers and brands that run multiple SKUs in small batches.
Precision is handled at the nozzle rather than through constant rework. The fill system adjusts to product viscosity, so a thin liquid and a thick paste can run through the same setup without changing pumps or rebuilding the product path. Operators can set target volumes and rely on the machine to hold tight tolerances, which reduces giveaway and eliminates the need to hand-adjust underfilled containers. Maintenance points are placed at the front of the machine, not buried behind guards or underneath conveyors, so daily checks and cleaning take minutes instead of a full shift. The overall result is a line that feels less like three machines bolted together and more like one tool built for the actual rhythm of a packaging room.
Contact Us
Contact Person: Tyson
Email: [email protected]
Tel/WhatsApp: +8613396971296
Website: https://www.wanyingmachinery.com